Fluid Controls

Services

Hose Assemblies

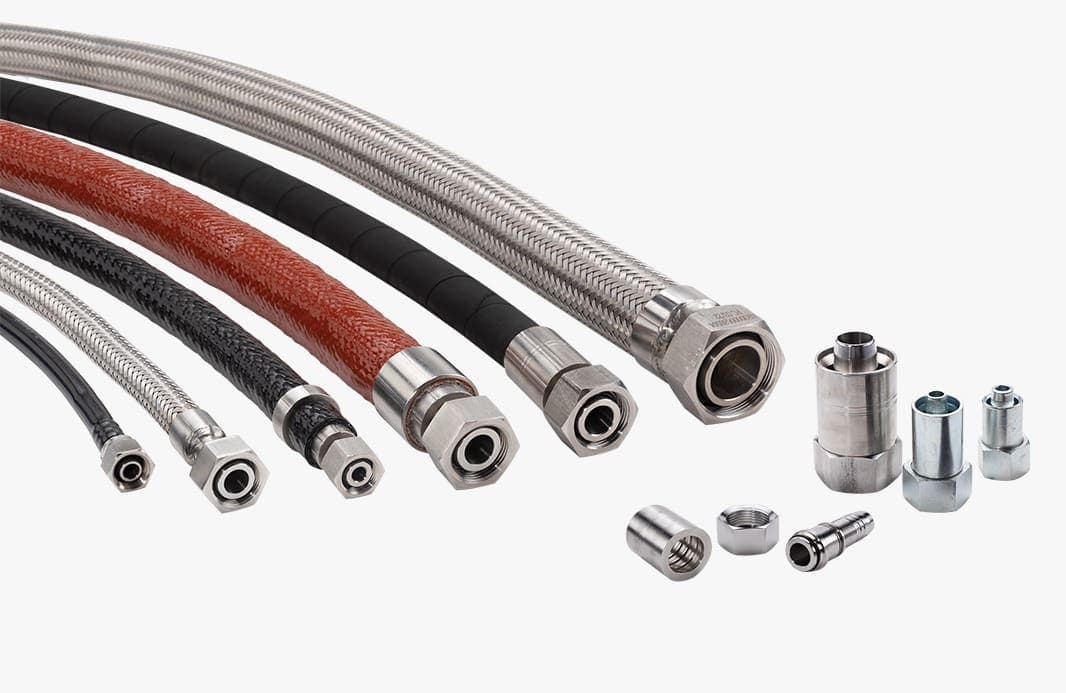
Hose, connectors and the crimp between them, supplied as one assembly under one part number and leak tested before despatch.

Highest pressure
450 bar
Rubber hose, crimped. PTFE to 300 bar, polyamide to 42 bar, metallic to 140 bar.
Temperature span
−60 to 350 °C
The metallic family. Rubber runs −54 to 125 °C, PTFE −54 to 250 °C, polyamide −40 to 100 °C.
Size range
1/4 to 4 in
Metallic hose. Rubber to 2 in, polyamide and PTFE to 1.1/4 in.
Hose families
4
Rubber, polyamide, PTFE and metallic: in stainless steel, carbon steel or brass.

Hose, connector and crimp are selected together for the application. The hose and the connector are each tested before assembly, and every finished assembly. Not a sample. Is leak tested before despatch. The figures quoted are the limit of each hose family rather than of a single assembly: rubber to 450 bar, PTFE to 300 bar, polyamide to 42 bar, metallic to 140 bar and up to 4 in.
The lifecycle

01
Engineering and hose selection
Your requirement is decoded and modelled to determine the right hose for the application. The first step, and the one the rest depends on.
02
Connector selection
Solid modelling and FEA settle the connectors and how they attach. Sleeves, springs and other accessories are decided once the hose, connector and crimp are configured.
03
Prototyping
A physical prototype is built and type tested before any bulk manufacture, to prove the joint does not leak and the assembly is fit for purpose.
04
Crimping and assembly
Hose cut to length and deburred on an automated skiving machine, then connectors crimped on a FINN Power electronic crimping machine with the die and load the joint calls for. Welding and brazing are available for metallic hose.
05
Tested before despatch
Every assembly is leak tested before it leaves. Burst, proof and leakage testing runs on our own Maximator hose test bench, to the standard the application cites.

On the assembly floor

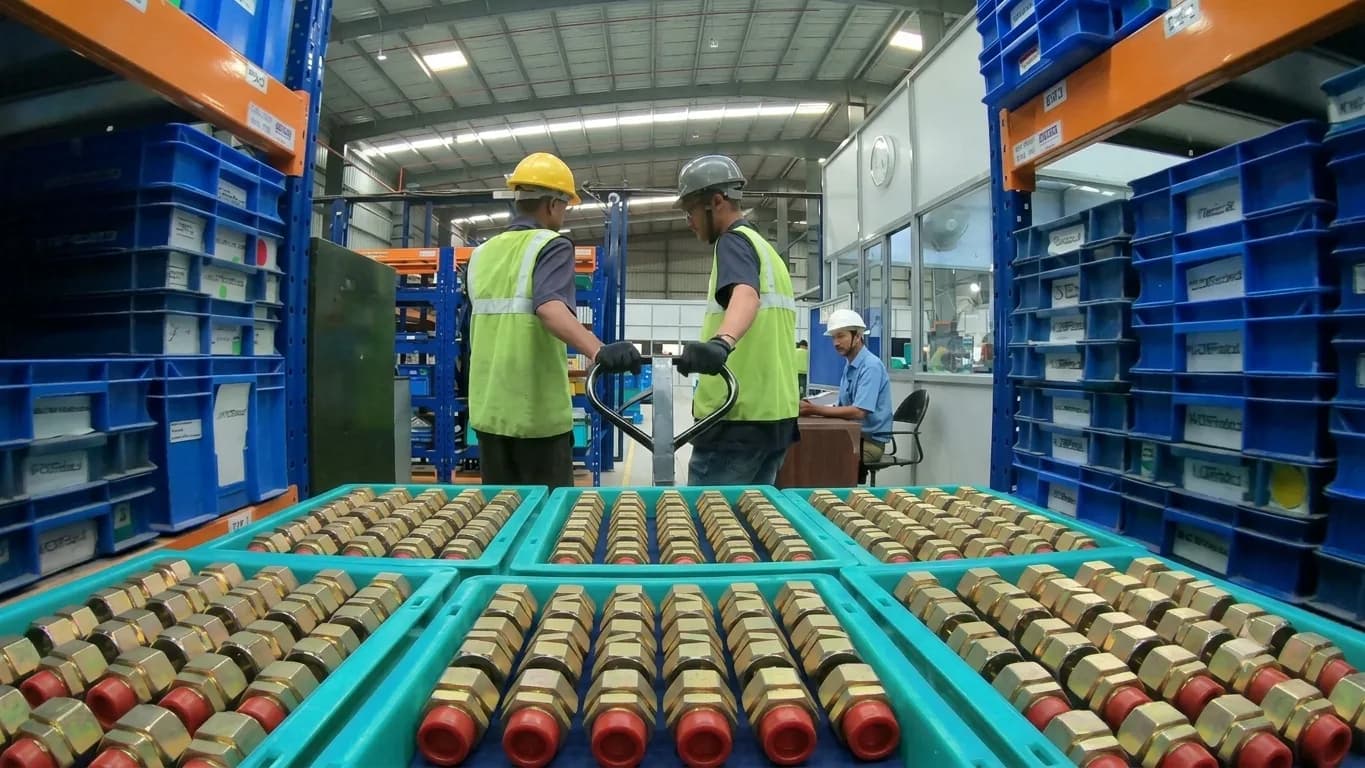
Plated connector bodies in tote bins on the assembly floor at Chakan, before they are crimped onto hose.
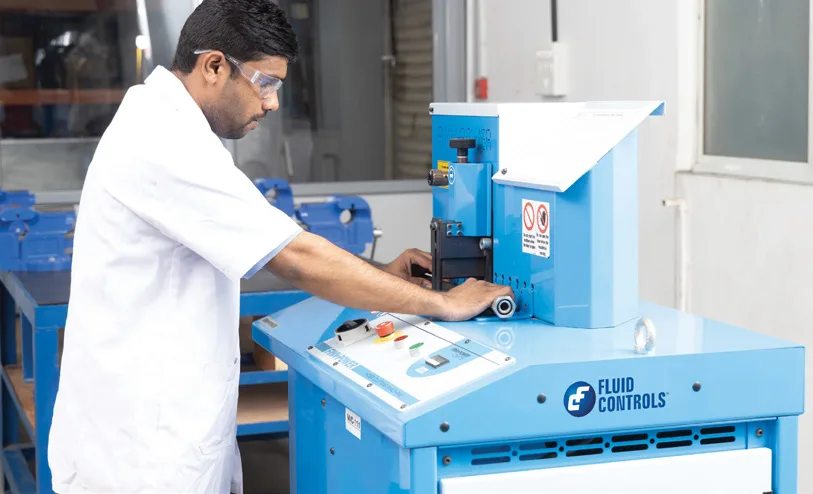
An operator at a Fluid Controls bench press, feeding a part into the die.
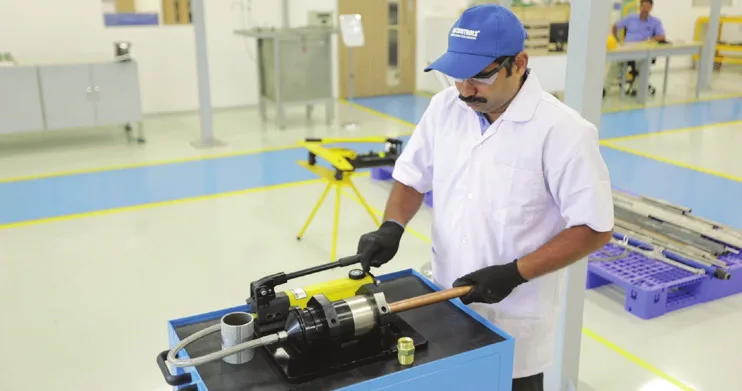
A hand pump raising pressure on a test piece in the laboratory at Chakan.

What we can show

  • Hose

    Hose bought in from manufacturers is tested to the customer's own specification. Burst, proof, leakage and impulse. Witnessed by Fluid Controls inspectors or by a third-party inspector.

  • Connectors

    Salt spray, plating, cyclic opening and closing, and leakage. Carbon steel connectors are zinc or zinc-nickel coated against corrosion.

  • The finished assembly

    Leak tested without exception before despatch, with burst and proof testing to the applicable standard on the Maximator bench.

We use essential cookies to run the site and, with your consent, analytics cookies to improve it. See our Privacy policy.